The modern industrial landscape relies heavily on the precision and reliability of high-pressure components, where the efficiency of a pump connector often determines the overall performance of complex machinery. In the casting and processing industry, creating these components requires a sophisticated balance of material science and advanced manufacturing techniques to ensure they can withstand extreme operational stresses.
Across global markets, the demand for specialized alloy parts has surged as industries shift toward more compact and powerful motor and pump designs. Achieving the necessary gas tightness and structural integrity in these parts is no longer just a technical requirement but a critical safety standard that prevents costly downtime and hazardous leaks in industrial environments.
By utilizing advanced extrusion casting methods, manufacturers can now produce a pump connector or motor shell that combines complex geometries with superior mechanical properties. This approach ensures that even parts with uneven wall thickness meet the rigorous tensile strength and hardness standards required for high-performance automotive and power accessories.
Structural Analysis of High-Precision Casting
Analyzing the process structure of high-precision parts, such as a pump connector or motor shell, reveals a complex interaction between geometry and fluid dynamics. These parts are often characterized by uneven wall thicknesses, where the middle section is thinner and the surrounding areas are thicker, necessitating a casting method that can handle varying densities without compromising structural integrity.
With profile sizes reaching approximately 420mm x 390mm x 150mm and casting thicknesses concentrating between 6-8mm, the structural complexity—including multiple holes and ribs—requires a high degree of precision. The use of ADC12 aluminum alloy allows for a balance of fluidity and strength, ensuring that the final product maintains its near-cylindrical shape while meeting strict industrial tolerances.
Indirect Squeeze Casting Methodology
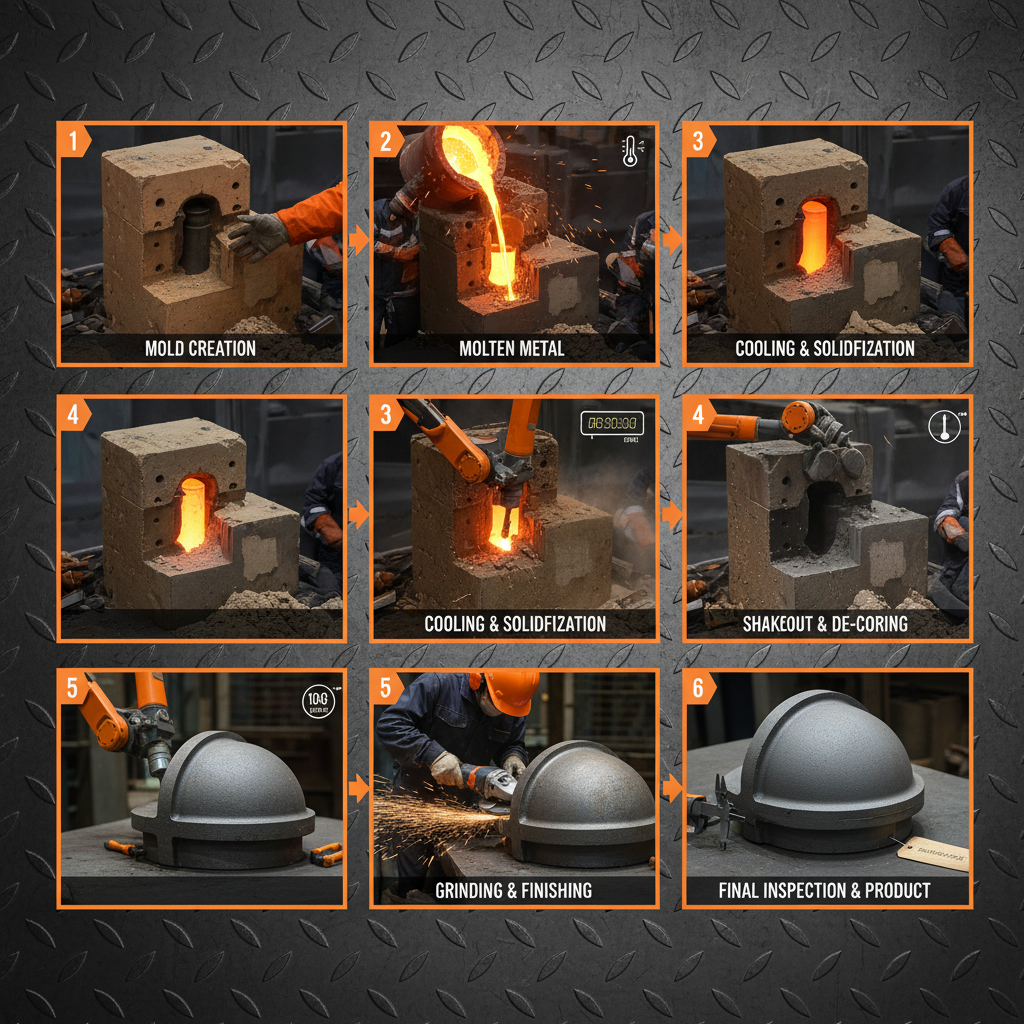
The selection of the extrusion casting method is pivotal in determining the ultimate quality of a pump connector. While direct squeeze casting is efficient for simple structures, indirect squeeze casting is far superior for complex parts. In this process, liquid metal is pushed into the mold cavity at a low speed with a large flow, then solidified under high pressure, which significantly reduces porosity.
One of the primary advantages of the indirect method is the short distance of the sprue and the large cross-section, which ensures sufficient pressure retention. This minimizes pressure loss during transfer, making it the ideal choice for components with intricate internal ribs and varying wall thicknesses that would otherwise be prone to shrinkage or voids.
For large and complex parts, a single-piece mold is typically employed to ensure uniformity. By carefully adjusting the pressure application position to the center, manufacturers can achieve rough symmetry even in non-axisymmetric parts, ensuring that the extrusion force is distributed evenly across the entire volume of the casting.
Material Integrity and Alloy Performance
The performance of a pump connector is directly linked to the mechanical properties of the alloy used. For industrial-grade shells and connectors, the tensile strength must meet or exceed 240MPa, with an elongation of at least 1.0% and a hardness of 80HBW to ensure durability under high-stress cycles.
ADC12 alloy is frequently selected due to its excellent fluidity and ability to form dense structures. When combined with extrusion casting, the liquid metal's fluidity allows it to fill the mold smoothly, while the subsequent plastic deformation under pressure improves the densification of the part, effectively eliminating the common pitfalls of uneven thickness.
Ensuring that the machined surfaces of the pump connector are free from cracks, cold segregation, and undercasting is paramount. These defects can lead to catastrophic failure in high-pressure environments, making the synergy between material selection and the solidification process the most critical factor in quality control.
Optimizing Gas Tightness and Leak Prevention
Gas tightness is a non-negotiable requirement for any high-performance pump connector. To validate this, parts are subjected to rigorous pressure tests, typically maintained at 1.6-2.0MPa for a duration of 3 minutes. Any leakage during this window indicates a failure in the casting density or the presence of microscopic pores.
To prevent shrinkage and liquid metal aggregation, manufacturers often incorporate grooves into the upper and lower end faces. This design promotes a more uniform wall thickness, allowing the liquid metal to fill the cavity smoothly and ensuring that the extrusion force is applied consistently across the part's surface.
Performance Comparison of Casting Methods for Pump Connector
Mold Design and Core Extraction Logic
The design of the mold for a pump connector must account for the challenges of deep and thin bores. To avoid the risk of core fracture due to rapid temperature rises and low strength, manufacturers often cast a shorter, thinner bore first and then achieve the final dimensions through precise machining.
Furthermore, the use of slider-extracted cores is essential for completing the complex surrounding shapes of the shell. To enhance mold service life and ensure smooth demolding, a draft slope of 1.5° is typically applied to the longitudinal non-machined surfaces, reducing friction and preventing surface damage.
Reducing Defects in Complex Geometries
One of the primary goals in producing a pump connector is the elimination of cold segregation and shrinkage. Because these parts often have uneven wall thicknesses, the liquid metal can tend to aggregate in thicker areas, leading to contraction voids.
By applying high pressure during the solidification phase, the plastic deformation of the metal fills these potential gaps. This densification process is what allows the part to meet strict gas-tightness requirements and ensures that the structural strength is consistent across both the thin 4mm and thick 28mm sections.
Continuous monitoring of the mold temperature and the precise timing of the extrusion force are also critical. This ensures that the ADC12 alloy remains in its optimal fluid state until the mold is completely filled, thereby preventing undercasting in the most intricate rib structures.
Manufacturing Standards for Industrial Components
Maintaining rigorous standards for the pump connector involves a multi-stage inspection process. From the initial analysis of the process structure to the final machining of the mold, every step is designed to mitigate the risk of structural failure and ensure adherence to international alloy standards.
The integration of indirect extrusion casting allows for a higher degree of repeatability and quality control compared to traditional methods. This consistency is vital for OEMs in the automotive and power sectors, where a single defective component can compromise an entire system's reliability.
Ultimately, the success of these components lies in the ability to transform complex theoretical parameters—such as tensile strength and gas tightness—into a tangible, high-performance product through meticulous engineering and advanced casting technology.
Core Technical Specifications for High-Pressure Casting Components
| Parameter Dimension |
Technical Requirement |
Testing Method |
Criticality Level |
| Tensile Strength |
≥ 240MPa |
Standard Tensile Test |
High |
| Gas Tightness |
1.6-2.0MPa / 3min |
Pressure Leak Test |
Critical |
| Material Hardness |
≥ 80HBW |
Brinell Hardness Test |
Medium |
| Wall Thickness |
4mm - 28mm |
Ultrasonic Measurement |
High |
| Surface Quality |
No cracks/shrinkage |
Visual/X-ray Inspection |
Critical |
| Draft Slope |
1.5° per side |
Geometric Verification |
Medium |
FAQS
Indirect squeeze casting allows for a smoother, low-speed flow of liquid metal and better pressure retention. This is crucial for complex parts with uneven wall thicknesses, as it significantly reduces porosity and shrinkage compared to direct casting, ensuring the component can withstand higher internal pressures.
Gas tightness is verified by applying a constant pressure of 1.6 to 2.0 MPa to the component. The part must maintain this pressure for at least 3 minutes without any detectable leakage, ensuring that the extrusion process has successfully densified the material.
Long, thin cores tend to heat up rapidly and lose strength, which can lead to core fracture during the casting process. To solve this, manufacturers often cast a short, thin bore first and then use precision machining to achieve the final depth and diameter.
ADC12 aluminum alloy is widely regarded as the optimal choice for these components. It provides excellent fluidity for filling complex molds and, when paired with squeeze casting, achieves a tensile strength of ≥ 240MPa and a hardness of ≥ 80HBW.
A draft slope (typically 1.5°) is essential for the smooth removal of the part from the mold. Without it, friction during demolding can cause surface scratches or structural deformation, which would compromise the quality of the non-machined longitudinal surfaces.
Yes, indirect extrusion casting is specifically suited for wall thicknesses between 1mm and 6mm. The high pressure applied during solidification ensures that even the thinnest sections are fully densified and free from defects.
Conclusion
The production of a high-performance pump connector requires a sophisticated integration of ADC12 alloy properties, indirect squeeze casting technology, and precision mold design. By focusing on gas tightness, structural densification, and the elimination of casting defects, manufacturers can produce components that meet the most demanding industrial specifications for tensile strength and durability.
Looking forward, the continued evolution of extrusion casting and the adoption of more rigorous testing standards will further enhance the reliability of pump and motor components. Investing in these advanced manufacturing processes not only reduces waste but ensures long-term operational safety and efficiency across the global industrial sector. Visit our website for more professional solutions: www.ydcastings.com